How to Use a Tap and Die Set
Overview
A tap and die set is used to create, repair and clean threads in metal.
A tap creates internal threads inside a drilled hole, allowing a bolt or screw to be installed.
A die creates external threads on a rod or bolt.
Threading is useful when building brackets, machine parts, fixtures, tools and custom workshop equipment.
The key to good threading is accurate drilling, correct tool selection, proper alignment and controlled pressure.
What You Need
- Tap and die set
- Tap wrench
- Die holder
- Drill press or drill
- Correct drill bits
- Cutting fluid
- Bench vice
- Caliper
- Center punch
- Deburring tool or file
- Safety glasses
- Appropriate work gloves when handling sharp parts
Before You Start
1. Identify the Thread
Determine the required:
- Thread diameter
- Thread pitch
- Thread standard
- Internal or external thread
Common thread systems include metric and imperial.
For example:
M8 × 1.25
means an 8 mm nominal diameter with a 1.25 mm thread pitch.
2. Choose the Correct Tap
A tap must match the desired thread.
Do not assume that every M8 tap produces the same thread. Different pitches require different taps.
3. Choose the Correct Drill Size
The hole must be drilled to the appropriate size before tapping.
For metric threads, the tap manufacturer’s recommended drill size should be used.
As a rough rule, the tapping drill diameter is often close to:
Nominal thread diameter − thread pitch
For M8 × 1.25:
8 − 1.25 = 6.75 mm
A standard recommended drill size may be selected according to the material and desired thread engagement.
Always check a reliable tap/drill chart for the exact application.
4. Secure the Workpiece
Clamp the material firmly in a vice.
The workpiece must not move while drilling or threading.
Safety
Sharp Tools
Taps and dies have extremely sharp cutting edges.
Handle them carefully and avoid touching the cutting flutes unnecessarily.
Secure the Workpiece
Never hold a small workpiece in your hand while drilling or tapping.
Use a vice or appropriate fixture.
Eye Protection
Wear safety glasses when drilling, tapping and removing metal chips.
Avoid Excessive Force
If a tap suddenly becomes difficult to turn, do not simply apply more force.
The tap may be misaligned, the hole may be too small, or chips may be trapped in the cutting flutes.
Broken Taps
Small taps can break if excessive force is applied.
A broken tap can be extremely difficult to remove from the workpiece.
Remove Chips Safely
Metal chips are sharp.
Do not wipe them away with bare hands.
Use a brush or suitable chip-removal method.
Cutting Fluid
Use an appropriate cutting fluid for the material and operation.
Lubrication can reduce friction, heat and tool wear.
How to Create an Internal Thread
Step 1 — Mark the Hole
Measure the required location.
Use a center punch to mark the center.
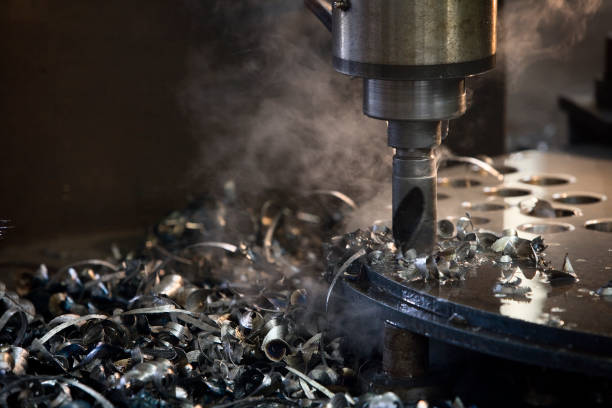
Step 2 — Drill the Hole
Drill the correct tapping-hole diameter.
A drill press is ideal because it helps keep the hole perpendicular.
Step 3 — Deburr the Hole
Remove sharp edges around the entrance to the hole.
A small chamfer can also make starting the tap easier.
Step 4 — Secure the Tap
Place the correct tap into the tap wrench.
Step 5 — Align the Tap
Position the tap as square to the surface as possible.
Alignment is critical.
A crooked tap can produce a poor thread or break.
Step 6 — Apply Cutting Fluid
Apply an appropriate amount of cutting fluid.
Step 7 — Start Cutting
Apply gentle downward pressure while turning the tap.
Once the tap has established the thread, maintain controlled rotation.
Step 8 — Break the Chips
For many conventional hand taps, periodically reversing the tap slightly can help break chips.
The exact technique depends on the tap design and material.
Do not force the tool.
Step 9 — Continue to the Required Depth
Continue until the required thread depth is reached.
For blind holes, make sure there is sufficient depth beyond the required usable thread.
Step 10 — Clean and Inspect
Remove the tap carefully.
Clean the hole and test it with the correct bolt or thread gauge.
Creating an External Thread
A die is used to create threads on a rod or suitable cylindrical workpiece.
Step 1 — Select the Die
Choose a die matching the required diameter and pitch.
Step 2 — Prepare the Rod
Cut the rod to the required length.
Make sure the end is reasonably square.
Step 3 — Create a Small Chamfer
A small chamfer on the end helps the die start more easily.
Step 4 — Secure the Rod
Clamp the rod securely in a vice.
Protect finished surfaces from unnecessary damage.
Step 5 — Align the Die
Place the die squarely on the end of the rod.
Poor alignment can produce crooked threads.
Step 6 — Apply Cutting Fluid
Lubricate the cutting area.
Step 7 — Start the Die
Apply controlled pressure while turning the die.
Step 8 — Break Chips
Periodically reverse the die slightly when appropriate to help clear chips.
Step 9 — Continue Cutting
Continue until the required thread length has been produced.
Step 10 — Clean and Inspect
Remove the die and clean the new thread.
Test it with the matching nut.
Applications
A tap and die set can be used for:
- Repairing damaged threads
- Creating mounting holes
- Making custom bolts
- Making threaded rods
- Building brackets
- Workshop fixtures
- Machine repairs
- Automotive repairs
- Custom tools
- Metal furniture
- Welding jigs
- Mechanical projects
Example Project — Adjustable Metal Bracket
A threaded adjustment mechanism can make a simple metal bracket much more versatile.
For example, a threaded hole can be created in one part of the bracket and a matching bolt used to adjust or secure another component.
Basic process:
- Mark the threaded-hole location.
- Center punch it.
- Drill the correct tapping size.
- Deburr the hole.
- Tap the thread.
- Clean the hole.
- Install the matching bolt.
- Test the adjustment.
Repairing a Damaged Thread
A tap can sometimes be used to clean and restore an existing thread.
For example, if a bolt no longer enters a threaded hole smoothly:
- Identify the thread size.
- Select the matching tap.
- Apply cutting fluid.
- Align the tap carefully.
- Slowly clean the damaged thread.
- Remove chips.
- Test with the correct bolt.
If the thread is severely damaged or stripped, simply running a tap through it may not restore the required strength. A larger thread, thread insert or replacement part may be necessary.
Useful Tricks
Make a Chamfer
A small chamfer on the entrance of a hole makes starting a tap easier and produces a cleaner thread entrance.
Use a Drill Press for Alignment
Even when tapping by hand, a drill press can help keep the tap perpendicular.
One useful method is to place the tap in a suitable chuck without powering the machine and use the machine’s spindle as an alignment guide while turning the tap manually.
Only use this technique when the setup is stable and appropriate for the machine.
Use the Correct Lubricant
Different metals benefit from different cutting fluids.
Do not assume one lubricant is ideal for every material.
Check the First Thread
When making multiple parts, inspect the first threaded hole before repeating the operation.
Keep Taps Organized
Store taps and dies together with their size markings visible.
A mixed-up set wastes time and can lead to using the wrong tool.
Pro Tips
- Always identify the thread size and pitch first.
- Use the manufacturer’s recommended tapping drill size.
- Keep the tap or die properly aligned.
- Secure the workpiece firmly.
- Use suitable cutting fluid.
- Apply controlled pressure.
- Clear chips regularly.
- Never force a tap that suddenly becomes difficult to turn.
- Chamfer holes before tapping when appropriate.
- Test threads with the correct mating component or gauge.
- Keep taps and dies clean and organized.
Common Beginner Mistakes
Using the Wrong Drill Size
A hole that is too small can make tapping extremely difficult and increase the chance of breaking the tap.
Poor Alignment
A crooked tap produces crooked threads.
Too Much Force
Forcing the tap is one of the fastest ways to break it.
No Lubrication
Dry cutting can increase friction and tool wear.
Wrong Thread Pitch
An M8 × 1.25 thread and an M8 × 1.0 thread are not interchangeable.
Tapping Too Deep
Blind holes need enough depth for the tap and chips.
Ignoring Chips
Accumulated chips can increase cutting resistance and damage the thread.
Beginner Practice Exercise
Take a piece of mild steel scrap.
Practice creating an M6 threaded hole:
- Mark the location.
- Center punch it.
- Drill the recommended tapping-hole diameter.
- Deburr the hole.
- Apply cutting fluid.
- Align the M6 tap.
- Cut the thread gradually.
- Clean the hole.
- Test it with an M6 bolt.
Then practice creating an external thread on a suitable metal rod using the matching die.
The goal is to learn alignment, controlled force, chip management and accurate thread selection.