How to Use a Metal Drill Press
Overview
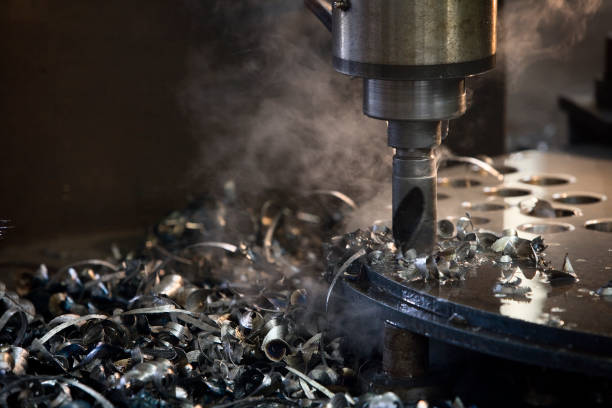
A metal drill press is a stationary machine designed for making accurate holes in metal.
Compared with a handheld drill, a drill press provides better control, repeatability and accuracy. It is especially useful when you need holes at a specific angle, depth or position.
A drill press can be used for drilling steel, aluminum and other suitable materials, as well as for countersinking, reaming and some other machining operations when the correct tooling is used.
What You Need
- Metal drill press
- Appropriate drill bits
- Cutting fluid
- Machine vice or suitable workholding
- Clamps
- Center punch
- Hammer
- Measuring tools
- Safety glasses
- Hearing protection
- Appropriate work clothing
- Deburring tool or file
Before You Start
1. Inspect the Machine
Check:
- Power cable and plug
- Drill chuck
- Chuck key
- Belts and guards
- Table
- Machine vice
- Emergency stop, if fitted
- Drill bit condition
Do not operate the machine if a safety guard or important component is damaged or missing.
2. Choose the Correct Drill Bit
Different metals require different cutting tools.
For general steel work, suitable high-speed steel (HSS) drill bits are a common choice.
For harder materials, specialized drill bits may be required.
Make sure the drill bit is sharp and suitable for the material.
3. Mark the Hole
Measure the position carefully.
Use a center punch to create a small indentation where the hole should be drilled.
This helps prevent the drill bit from wandering when it starts cutting.
4. Secure the Workpiece
Place the metal in a machine vice or secure it with appropriate clamps.
Never hold the workpiece by hand while drilling.
A drill bit can catch the material and spin it violently.
5. Set the Speed
Drill press speed depends on:
- Drill diameter
- Material
- Drill bit type
- Cutting conditions
Larger drill bits generally require lower speeds than smaller drill bits.
Use the machine manufacturer’s speed recommendations whenever available.
Safety
Secure the Workpiece
Always secure metal before drilling.
A loose piece of metal can become a dangerous projectile if the drill catches it.
Keep Hands Away From the Drill
Never place your fingers near the rotating drill bit.
Wait until the machine has completely stopped before removing chips or adjusting the workpiece.
Remove the Chuck Key
After tightening the drill bit, remove the chuck key before starting the machine.
Leaving it in the chuck can turn it into a projectile.
Eye Protection
Wear suitable safety glasses.
Metal chips can be extremely sharp and can travel at high speed.
Avoid Loose Clothing
Keep sleeves, jewelry, long hair and other loose objects away from rotating parts.
Do Not Remove Chips by Hand
Never brush away chips while the drill is rotating.
Stop the machine and use a suitable brush or chip-removal tool.
Cutting Fluid
Cutting metal generates heat.
Use an appropriate cutting fluid or lubricant when required for the material and drilling operation.
Do not apply liquids in a way that creates an electrical hazard.
Hot Metal
Recently drilled metal and chips can become extremely hot.
Allow them to cool or use appropriate tools to handle them.
How to Use a Metal Drill Press
Step 1 — Mark the Hole
Measure the desired location and mark it with a center punch.
For multiple holes, use a ruler, square, template or other suitable measuring method.
Step 2 — Install the Drill Bit
Insert the correct drill bit into the chuck.
Tighten it securely.
Remove the chuck key.
Step 3 — Secure the Metal
Clamp the workpiece in a machine vice or with suitable clamps.
Make sure the area to be drilled is positioned directly under the drill.
Step 4 — Set the Table
Adjust the drill press table to the correct height and position.
Make sure there is enough clearance below the workpiece.
Step 5 — Set the Speed
Choose an appropriate spindle speed for the drill diameter and material.
Use the manufacturer’s recommendations when available.
Step 6 — Start the Machine
Stand in a stable position.
Start the drill press and allow it to reach its normal operating speed.
Step 7 — Start Drilling
Lower the drill slowly into the material.
Apply steady pressure.
Do not force the drill.
Step 8 — Use Cutting Fluid
When appropriate, apply cutting fluid to the drilling area.
This can reduce heat and improve tool life.
Step 9 — Clear Chips Safely
Stop the machine when necessary and remove chips using a brush or suitable tool.
Do not touch sharp chips with bare hands.
Step 10 — Finish the Hole
When the drill breaks through the material, reduce pressure carefully.
This helps prevent the drill from suddenly grabbing the workpiece.
Stop the machine and inspect the hole.
Drilling a Large Hole
When making a large hole, drilling directly with a very large bit can put unnecessary load on the machine and tool.
A useful technique is to create a smaller pilot hole first.
For example:
- Mark the center.
- Center punch it.
- Drill a small pilot hole.
- Increase the drill size gradually if appropriate.
- Finish with the required diameter.
The exact procedure depends on the material, drill size and machine.
Drilling Thin Sheet Metal
Thin sheet metal can grab a conventional drill bit as it breaks through.
To improve control:
- Secure the sheet firmly.
- Use an appropriate drill bit.
- Support the material properly.
- Reduce feed pressure as the bit breaks through.
- Consider tooling specifically designed for sheet metal when appropriate.
Creating a Precise Hole Pattern
A drill press is excellent for making repeated holes.
For example, you could make a metal bracket with four mounting holes.
- Measure the hole positions.
- Create a template if several identical parts are required.
- Center punch every location.
- Secure the workpiece.
- Drill each hole.
- Check the dimensions.
- Deburr the holes.
For repeated production work, a dedicated jig can make the process faster and more consistent.
Countersinking
A countersink creates a conical recess around a hole.
This can allow a countersunk screw to sit flush with the metal surface.
Use a suitable countersink tool and controlled feed pressure.
Do not remove excessive material.
Deburring
Freshly drilled holes often have sharp edges.
After drilling:
- Stop the machine.
- Remove the workpiece.
- Use a deburring tool, countersink or file.
- Remove sharp edges.
- Inspect the hole.
Deburring makes the part safer to handle and can improve assembly.
Applications
A metal drill press can be used for:
- Metal brackets
- Steel frames
- Welding fixtures
- Tool holders
- Machine parts
- Shelving systems
- Metal furniture
- Mounting plates
- Hinges
- Workshop equipment
- Custom mechanical parts
- Repair work
- Repeated hole patterns
Example Project — Metal Tool Holder
A simple wall-mounted tool holder is a good beginner project.
Step 1
Cut a piece of flat steel or suitable metal.
Step 2
Mark the mounting holes.
Step 3
Center punch the marks.
Step 4
Clamp the metal in the drill press.
Step 5
Drill the holes.
Step 6
Deburr the holes.
Step 7
Clean and finish the metal.
Step 8
Mount the finished holder using appropriate fasteners.
This project teaches measuring, center punching, workholding, drilling and deburring.
Useful Tricks
Use a Center Punch
Even a small indentation can make a big difference in keeping the drill centered.
Start With a Pilot Hole
For larger holes, a smaller pilot hole can make drilling easier and more controlled.
Use a Sacrificial Backing Board
When drilling through sheet metal, a suitable backing material can help support the workpiece and reduce deformation.
Make sure the backing material is securely positioned and appropriate for the operation.
Mark the Required Depth
If you do not need to drill completely through the material, mark the desired depth on the drill bit with tape or use the drill press depth stop.
Use a Jig for Repeated Parts
If you are making ten identical brackets, don’t measure every hole ten times.
Create a simple jig or template that positions the workpiece consistently.
Check Your First Part
When making multiple parts, drill and inspect one piece first.
Once you know the dimensions and setup are correct, produce the remaining pieces.
Pro Tips
- Use sharp, appropriate drill bits.
- Keep the workpiece firmly secured.
- Use the correct spindle speed.
- Use cutting fluid when appropriate.
- Start with a center punch.
- Use pilot holes for many large-hole operations.
- Reduce pressure as the drill breaks through.
- Stop the machine before clearing chips.
- Deburr every finished hole.
- For repeated parts, use a jig or template.
- Measure your first finished part before making a whole batch.
Common Beginner Mistakes
Drilling Without Clamping
This is one of the most dangerous mistakes.
Never rely on your hand to hold the workpiece.
Using Excessive Speed
High speed can generate excessive heat and rapidly damage a drill bit.
Pushing Too Hard
Excessive pressure can break the drill or damage the workpiece.
Not Using Cutting Fluid
For many metal-drilling operations, proper lubrication can significantly improve cutting performance and tool life.
Forgetting the Chuck Key
Always remove it before starting the machine.
Ignoring Chips
Long, sharp metal chips can cause serious cuts.
Keep the machine stopped when removing them.
Poor Measurements
A perfectly drilled hole in the wrong location is still a failed part.
Measure carefully before drilling.
Beginner Practice Exercise
Take a piece of scrap mild steel and practice:
- Measuring a hole position.
- Center punching the location.
- Selecting an appropriate drill bit.
- Securing the metal in a vice.
- Setting an appropriate speed.
- Drilling a small hole.
- Enlarging it with a larger drill.
- Deburring the finished hole.
- Measuring the final diameter.
Then try making a simple row of equally spaced holes.
The goal is to develop accuracy, workholding and control rather than simply making holes quickly.